Off-the-shelf is cheaper. That’s the conventional wisdom.
Why “spend the money” on a custom project when you can just work with something pre-made, right? Wrong.
We often surprise our clients with this truth — and then we break down the math.
Bottom line, it is cheaper and more efficient to design a custom case from scratch than to adapt an off-the-shelf solution to their device.
Purchasing a pre-made case, may seem like the most convenient option. However, a custom-designed case in most of cases proves to be the more cost-effective choice in the long run, especially beyond certain quantity, unique requirement, or specialized industries.
Let’s dive into why!
Custom Equipment Cases Save You Money on Features You Don’t Need
Off-the-shelf cases are designed to cater to a broad audience, which often results in extra features or materials that your project may not require. Custom designed cases allow you to include only what you need, eliminating wasted components and reducing costs.
For example, maybe you need a custom equipment case for your sales demo materials. Does a case like this really require high-level water resistance, shock absorption or the kinds of locks you might find on an EMS device case? Highly unlikely. But with an off-the-shelf, you may be getting those features anyway, whether you want them or not. A few cents more for these features really adds up when you purchase at scale.
(Curious about whether you require waterproofing? We have a blog about that here).
Custom Equipment Cases Don’t Need Modifications
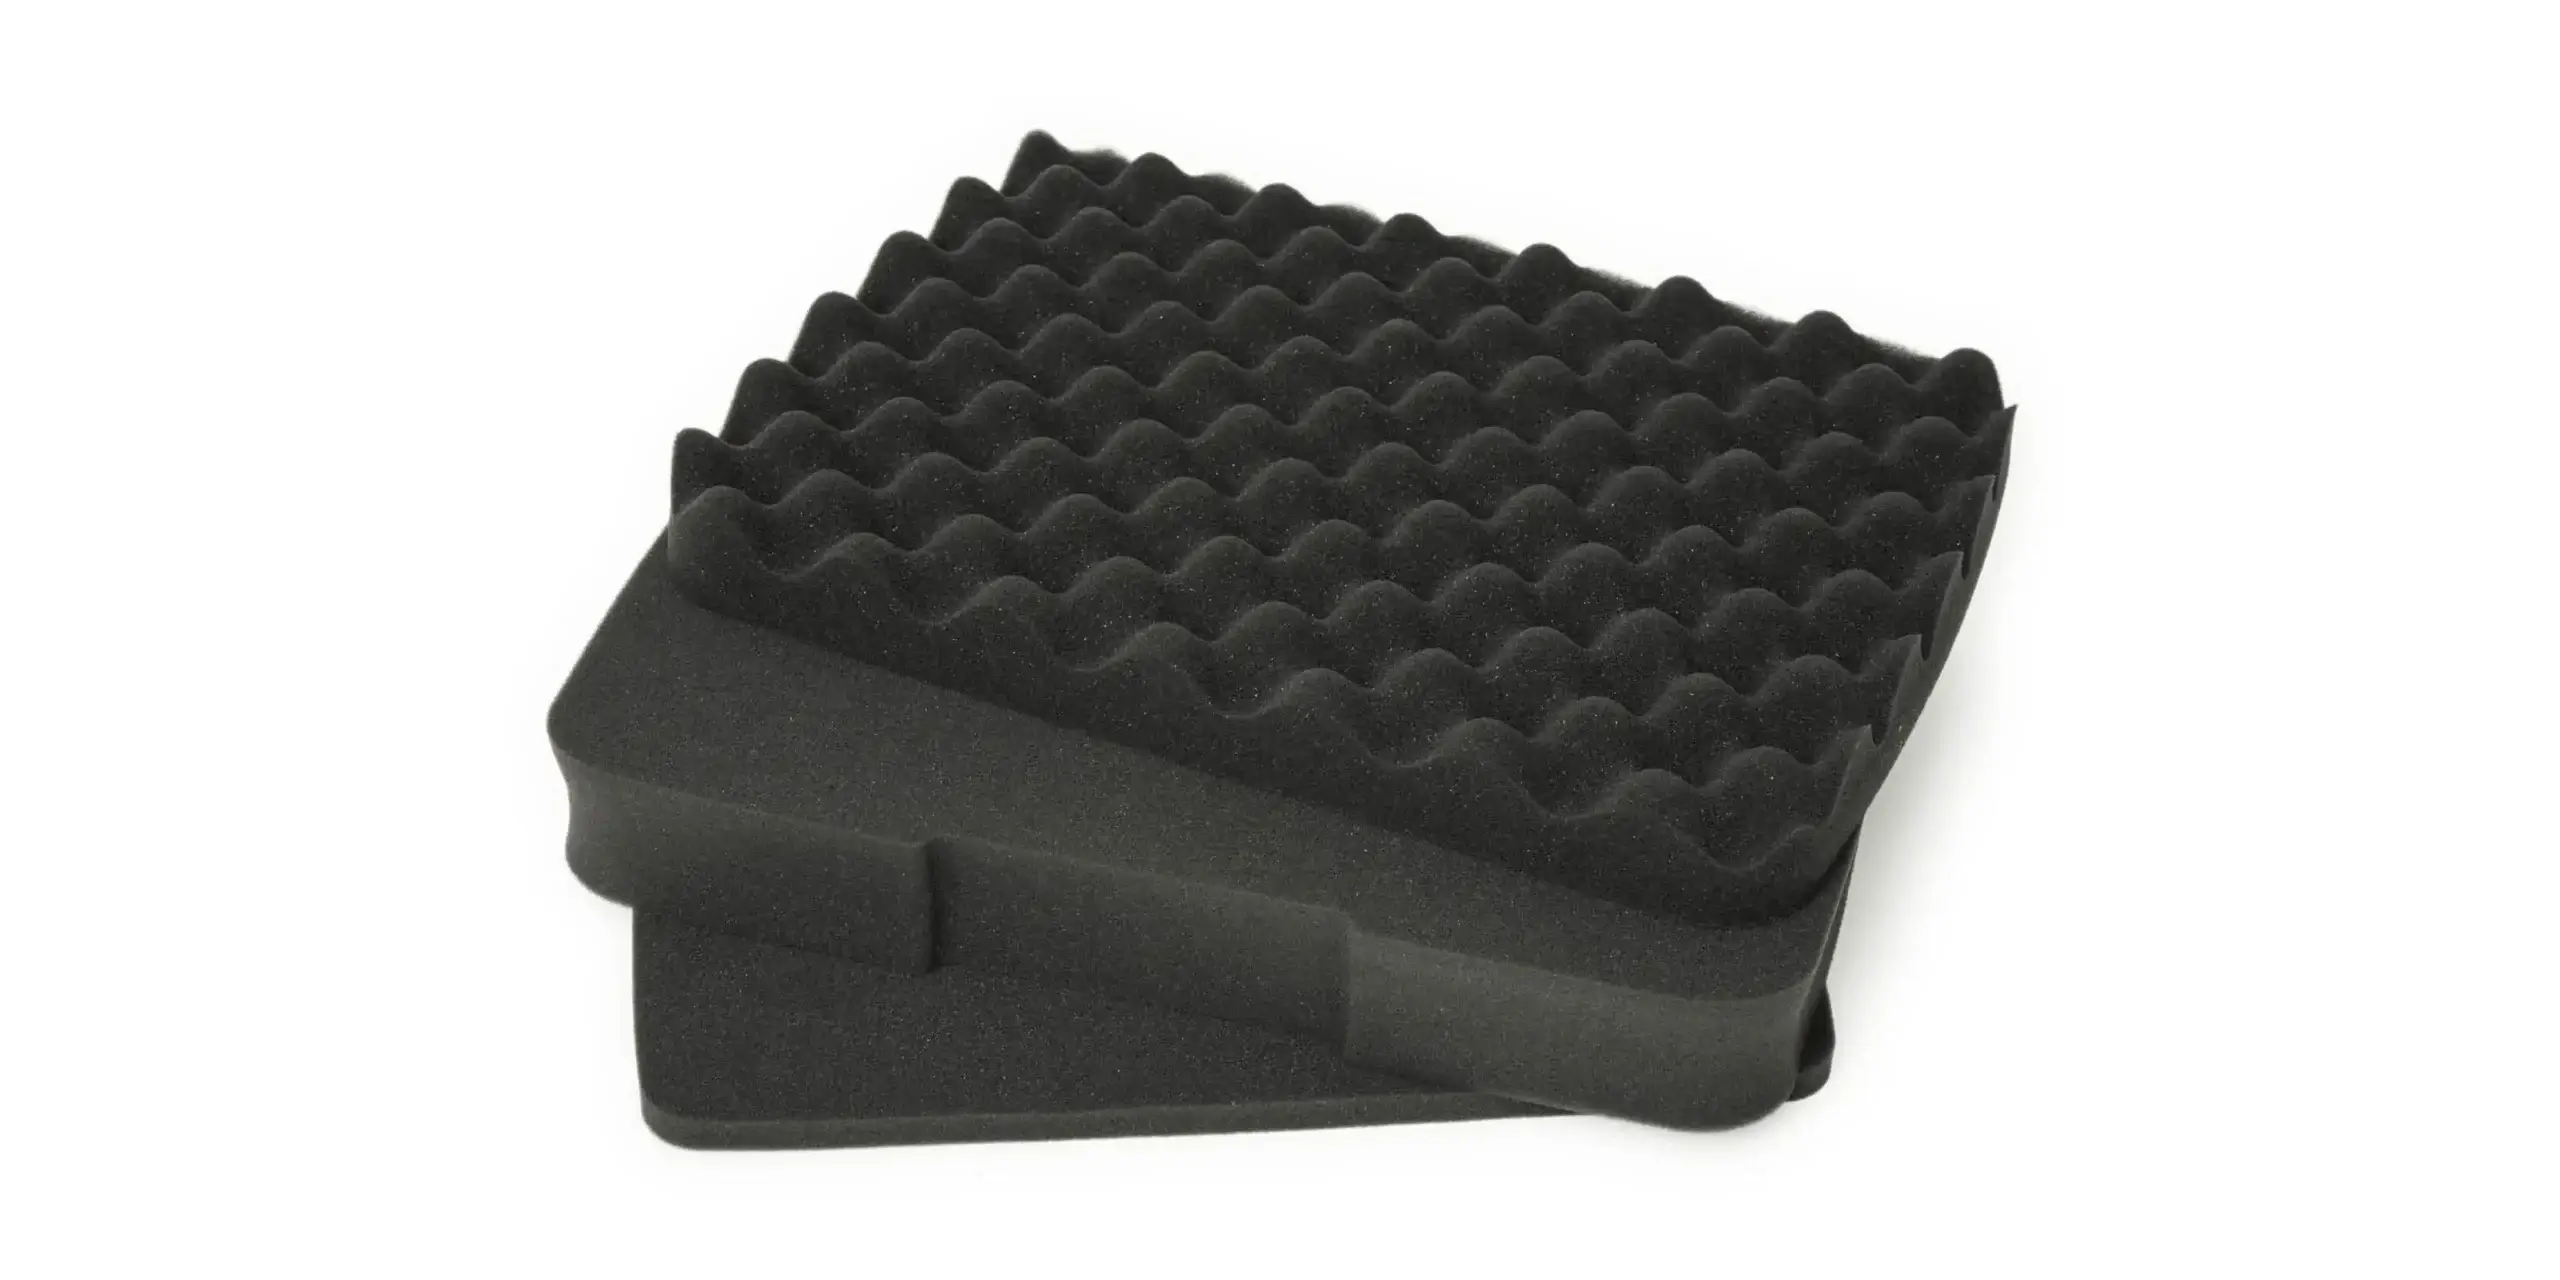
Off-the-shelf solutions often require additional modifications to meet your unique requirements, adding to the total cost. Examples of modification costs include cutting holes for connectors, resizing compartments, or adding reinforcements and modifications such as custom foam inserts. There’s a wide range of modifications you might need, and no “one-size-fits-all” solution, and so you’ll be faced with the cost of making it work. Custom designs, on the other hand, eliminate the need for retrofitting since the case is built with your specifications in mind.
Custom Cases Benefit from Scalability
Counterintuitive though it may sound, scaling your own design can really reduce the cost per unit significantly as production. Manufacturing in bulk allows you to take advantage of economies of scale, something that’s not always possible with off-the-shelf solutions.
Custom Solutions Save You on Brand Markups
Many off-the-shelf solutions come with premium pricing due to the brand name attached to them. These markups are unavoidable when you’re purchasing to retrofit. Custom cases bypass this markup, as you’re paying directly for materials, labor, and design, not the reputation of a specific manufacturer.

Custom Equipment Cases Put You in Charge of Materials Selection
Off-the-shelf cases often use generic materials to accommodate a wide range of applications, which might not align with your project’s requirements. Designing your own case gives you the freedom to choose the most suitable materials for your specific requirements and budget. You can specify and select the materials that ensure the level of protection your valuable equipment needs.
Bulk Custom Solution Purchasing Reduces Shipping and Handling Costs
Off-the-shelf cases, especially those sold by distributors, may incur high storage, shipping and handling fees due to their bulk or weight. With custom design, you can produce your custom cases, further cutting down storage and handling fees. Not to mention superior quality control and a more deep understanding of the environments your custom orders pass through on their way to you and your clients’ doorstep.
 Custom Equipment Cases are a Long-Term Investment vs. a Quick Fix
 Custom Equipment Cases are a Long-Term Investment vs. a Quick Fix
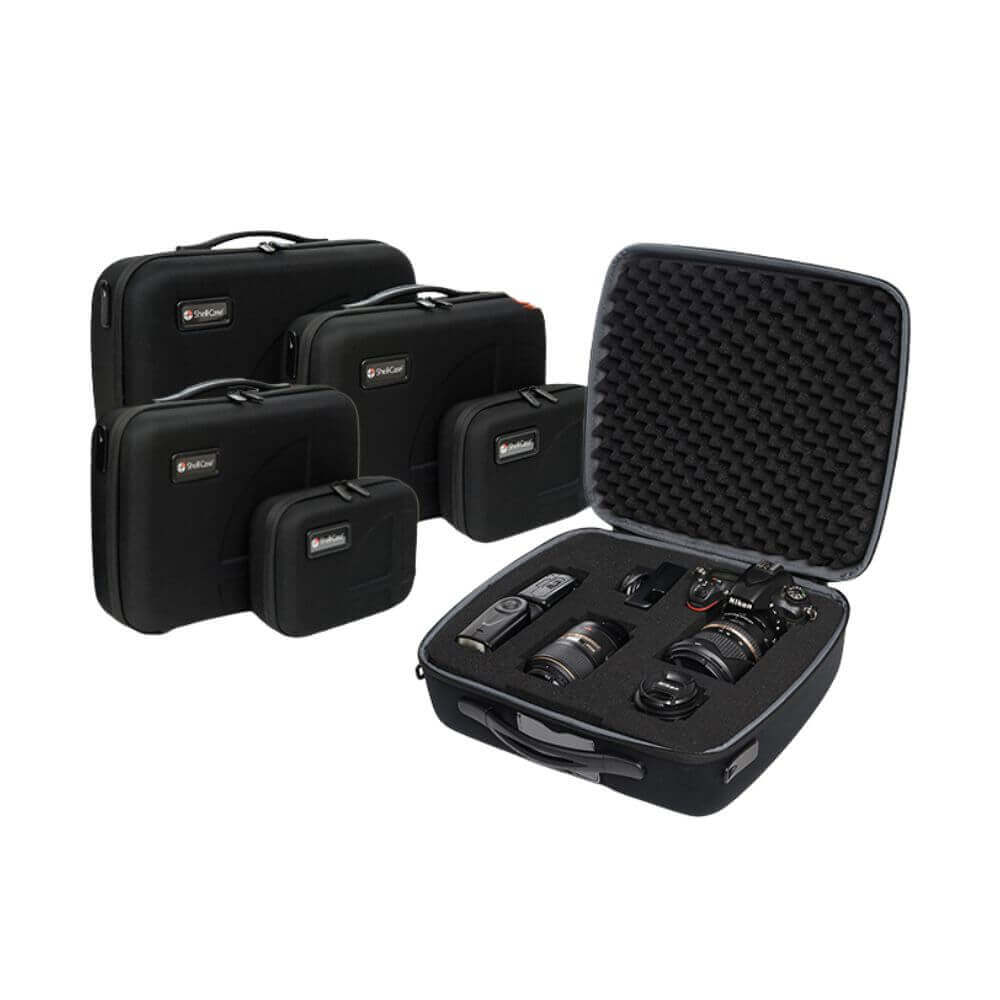
Off-the-shelf cases might seem cheaper upfront but could cost more in the long run if they don’t perform as expected. A custom-designed case ensures durability, functionality, and efficiency, reducing the need for replacements or upgrades and increasing customer satisfaction. Over time, the initial investment in designing a case can pay off through reduced maintenance and improved performance – ensuring protection for your valuable items and a positive user experience over the long haul.
Tailored Aesthetics for Your Custom Solution at a Lower Price
Custom cases let you dictate the design, select from a wide range of color options, and finish, often at a lower cost than customizing an off-the-shelf option. Branding elements, such as logos or unique designs, can be incorporated without the high fees charged by pre-made case manufacturers. This delivers higher value to your end user, and makes your sales team’s job easier too!

Custom Equipment Cases Meet Specific Regulatory Requirements
 In industries like aerospace, healthcare, or defense, regulatory compliance is crucial, and pre-made cases may not meet the necessary standards and require significant retrofitting investment to build in the custom protective solution your sensitive equipment may need. Custom designs ensure compliance from the outset, avoiding costly modifications or replacements.
Designing your own custom equipment case might seem like a complex and expensive endeavor, but it often proves to be the more economical choice, especially for projects with specific needs or superior protection demands. With design to execution, you avoid unnecessary costs associated with generic, one-size-fits-all solutions and give yourself peace of mind knowing that you’re tailoring the design, material, and production process to your exact requirements. Whether you’re scaling production or meeting niche demands, a custom-designed case is a smarter investment in both quality and cost-efficiency, that ensures you build and maintain your company’s reputation for excellence for years to come.
To learn more about how to produce your own custom equipment case, reach out to the Shell-Case team now by filling out this form.